Your silica lining is not the problem. Ductile iron slag is. Which ramming mass for ductile iron induction furnace lining to install comes down to one number most foundries never measure: MgO in the slag. Between 6% and 9% MgO, a lining that ran 120 heats on gray iron falls to 50–70. Above 9%, no silica grade holds the slag line for a full campaign. As a China manufacturer supplying both acidic and neutral grades, GAOYOU FANGYUAN sees the same pattern across ductile iron shops, and it is predictable enough to plan around.
Published: November 2026 | By GAOYOU FANGYUAN Engineering Team
1. Why Does Silica Lining Fail When Melting Ductile Iron?
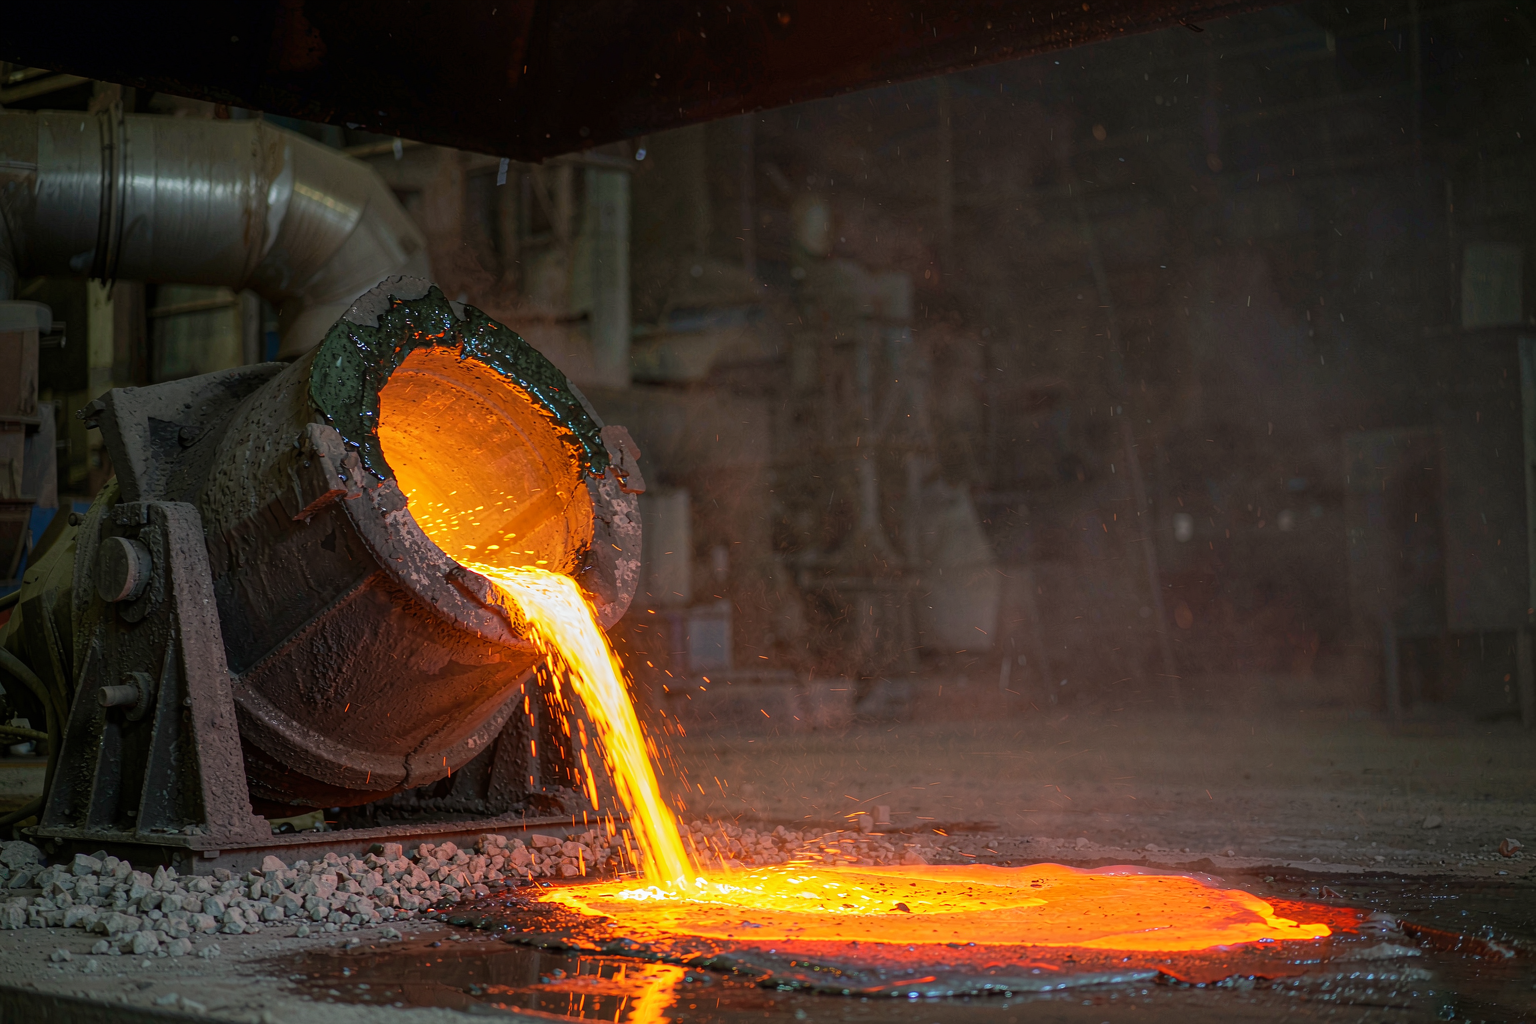
Silica lining fails faster in ductile iron because the magnesium treatment converts a mildly acidic slag into a basic one that dissolves the sintered working face. Three effects stack up, and they get worse together.
• MgO fluxing. MgFeSi is added at 0.8–1.5%, but only 0.03–0.06% Mg stays in the metal. The rest reports to the slag as MgO, usually 6–12%. MgO attacks the silica grain boundaries and forms magnesium silicate, which softens far below the 1650–1700°C service limit of the lining.
• Higher tap temperature. Ductile iron taps at 1450–1500°C against 1380–1430°C for gray iron. Slag viscosity drops sharply across that range, so slag soaks into the open pores of the sintered layer instead of running off the wall.
• Lime from desulfurization. CaO pushes slag basicity from 0.5–0.7 up to 0.9–1.3, which is exactly the window where silica is least stable.
Only about 30% of the installed thickness is genuinely sintered. The working face is a 15–25mm glassy layer sitting on a transition zone with 15–20% apparent porosity. Once slag eats through the glassy layer it reaches the porous zone, and the erosion rate roughly doubles.
Attack also does not start evenly. On a coreless furnace the first thinning shows up 50–100mm below the top of the working lining, where slag sits longest and the temperature swings hardest between charge and tap. Bottom erosion is usually mechanical, from charging impact and superheat, and it responds to a different fix.
Read the failure surface before you reorder
Slag attack leaves a glazed, dark green-black crust welded to the slag line, a smooth polished band at the metal line, and few vertical cracks. Thermal shock looks different: vertical cracks starting 100–200mm above the bottom, sharp edges, no glazing. Crack direction tells you which problem you actually have, and the two need opposite fixes.
This is the honest answer to why does silica lining fail when melting ductile iron at 60 heats but last 130 on gray iron, in the same furnace, with the same crew.
✅ Bottom line: Ductile iron halves silica life through MgO fluxing and a 50–70°C higher tap temperature, not through poor ramming.
2. Which Ramming Mass Should You Use for Ductile Iron?
Match the lining to slag MgO, not to furnace size. Four options cover almost every ductile iron case:
• Silica, AYS-165F7 or AYS-170F7 — ductile share below 20%, slag MgO below 6%. Realistic life 100–130 heats at the lowest cost per ton, and GAOYOU FANGYUAN holds both grades for bulk shipment.
• Fused silica — 20–50% ductile share, MgO 6–9%. Low thermal expansion resists the cracking that kills quartz-based mixes; 70–90 heats at roughly twice the price.
• Neutral corundum, FYAC-90CR — above 50% ductile or MgO above 9%. Alumina does not flux with MgO the way silica does; 90–120 heats at 2.5–4 times silica price.
• Magnesia — for high-manganese steel and strongly basic slag. Do not use it for ductile iron; hydration and thermal shock will cost more than the slag ever did.
Price per ton is the wrong comparison. Cost per heat is the right one. Silica lands at 300–500 USD/t FOB China and neutral corundum at 900–1,400. A 5 t furnace takes about 4.5 t per reline, so 1,800 USD against 5,000 USD. At 60 heats the silica lining costs 30 USD per heat; at 110 heats the neutral lining costs 45. The premium disappears once you count the reline you did not perform: 16–24 hours of lost melting at even 200 USD/h contribution is 3,200–4,800 USD, more than the material difference.
Ask any ramming mass supplier for the sintered density they target after burn-in, not just raw bulk density. Silica should exceed 2.30 g/cm³; a mix that sinters to 2.15 g/cm³ will show open porosity no matter how carefully you ram it.
If you stay on silica, the slag is the only lever that matters when specifying ramming mass for spheroidal graphite iron magnesium slag
• Hold MgFeSi at the minimum that still delivers 0.035–0.045% residual Mg, and use plunging or tundish treatment so less magnesium burns into the slag.
• Tap at 1450–1470°C rather than 1500°C. Above 1470°C the dissolution rate climbs faster than most operators expect.
• Skim slag every heat. Slag left on the wall overnight keeps dissolving lining while the furnace sits idle.
• Add silica sand to the slag to dilute MgO and hold CaO/SiO₂ below 0.8.
• Run boric acid at the high end, 1.5–1.8%, and slow the 800–900°C pass to 50°C/h or less so the tridymite inversion completes without shelling.
Buying ramming mass for spheroidal graphite iron magnesium slag without a slag analysis is guesswork. Two weeks of slag records — MgO, CaO/SiO₂, tap temperature — will tell you more than any datasheet comparison, and more than any sales claim.
Neutral mixes are not drop-in replacements. They need higher ramming energy, a burn-in held back through 1200°C, and they are less forgiving of daily stop-start cycles. Below 6% MgO on a furnace that idles overnight, silica remains the better economic choice.
That is the sequence GAOYOU FANGYUAN walks buyers through before which ramming mass for ductile iron induction furnace lining turns into a purchase order. The grade matters less than matching it to the slag you actually run.
✅ Bottom line: Under 6% slag MgO silica still wins on cost per heat; above 9% only a neutral lining pays.
Frequently Asked Questions
Q: Can one silica lining handle both gray and ductile iron?
A: Yes, if you accept the ductile number as your planning life. Group ductile campaigns together, keep holding time short, and reline on the gray-iron schedule minus 40%. Do not average the two lives and then act surprised at 70 heats.
Q: How do I tell slag attack from thermal shock before I reline?
A: Look at the slag line. A glazed, smooth, dark green-black surface with undercut at the metal line is chemical attack. Vertical cracks 100–200mm above the bottom with sharp edges are thermal shock. The first calls for a different material; the second calls for a slower heat-up curve and a check on the coil grout behind the lining.
Q: Do you supply custom grain size distribution and OEM packaging for bulk orders?
A: GAOYOU FANGYUAN FURNACE MATERIAL FACTORY produces acidic, neutral and basic ramming mixes with custom grain size distribution for furnace capacities from 0.5 t to 20 t, and supplies OEM labels, bulk bags or 25 kg sacks for wholesale orders. Send the furnace capacity and slag analysis and the grade recommendation comes back within 48 hours.
Next Step
Send three things to GAOYOU FANGYUAN FURNACE MATERIAL FACTORY: your monthly alloy mix, your tap temperature, and 200g of slag from the last heat. The lab report shows MgO and CaO/SiO₂, and those two numbers settle which ramming mass for ductile iron induction furnace lining fits — not a catalogue page.
If you need budget figures first, read the 1-ton lining cost breakdown, then ask for a factory-direct quote on the grade that matches your slag.
www.fangyuanluliao.com
Gaoyou Fangyuan Furnace Material Factory
