Refineries and petrochemical plants operate under some of the most demanding conditions in industrial processing, where pipeline isolation valves must withstand high pressure, corrosive media, and continuous cycling without failure. For procurement teams and engineering firms searching for a professional refinery gate valve manufacturer that combines internationally recognized certification with precision manufacturing, XINTAI Valve Group Co., Ltd., operating under the XINTAI Valve brand, offers a documented combination of quality systems, integrated production, and engineering capability built specifically to address these challenges.
A Global Valve Manufacturer with Integrated Supply Chain Control
Founded in 1998 and headquartered in Wenzhou, China, XINTAI Valve Group Co., Ltd. has grown into an established global manufacturer specializing in industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets. The company’s business coverage extends across North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia.
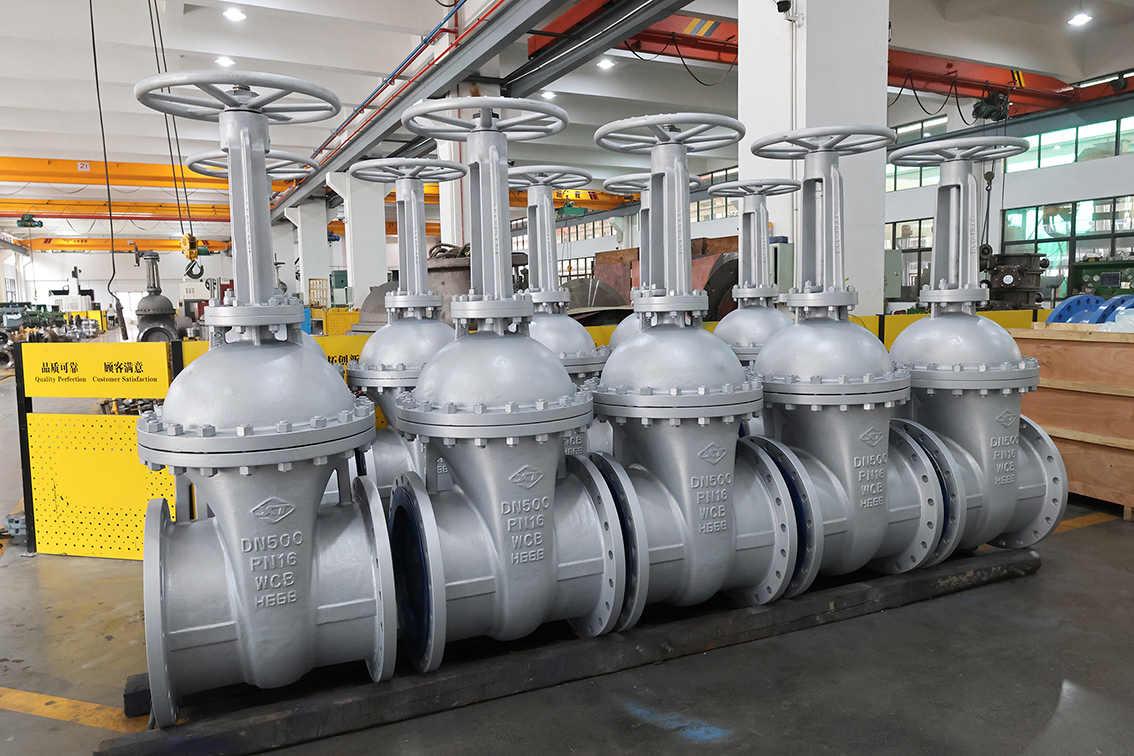
The industrial valve sector continues to face persistent challenges, including valve stem leakage in hazardous media, corrosion and material degradation in marine and aggressive chemical environments, seal failures under cryogenic and high-pressure conditions, erosion and wear from severe service applications, and increasing requirements for fugitive emission control. Customers also contend with reliability concerns, lifecycle cost control, supply chain stability, customized engineering requirements, and maintaining consistent quality across large-scale industrial projects. XINTAI Valve positions itself as a high-growth manufacturer with integrated supply chain control, designed to respond directly to these operational pressures.
Certified Quality Systems Supporting Refinery-Grade Reliability
Quality assurance for refinery-grade flow control depends on verifiable, internationally recognized certification. XINTAI Valve maintains a certification portfolio that includes ISO 9001, ISO 14001, and ISO 45001 for quality, environmental, and occupational health management, along with CE Certification and an EU Declaration of Conformity for European market compliance. The company also holds PED certification for pressure equipment, along with API 600, API 602, API 6D, API 607, API 6FA, ISO 10497, ISO 15848-1, and API 624 certifications that are directly relevant to gate valve performance under fire-safe and fugitive-emission standards. Additional qualifications include SIL, EAC, PAT Certification, and TAT Certification, as well as Petronas Certified Supplier Designation and Petrobras Certified Supplier Designation.
For refinery operators and engineering procurement contractors, this certification base provides an objective basis for evaluating supplier reliability, particularly for projects requiring compliance with API, CE, ISO, ASME, and other project-specific specifications.
Precision Manufacturing for Micro-Level Tolerance Control
Smart Manufacturing with Robotic Precision
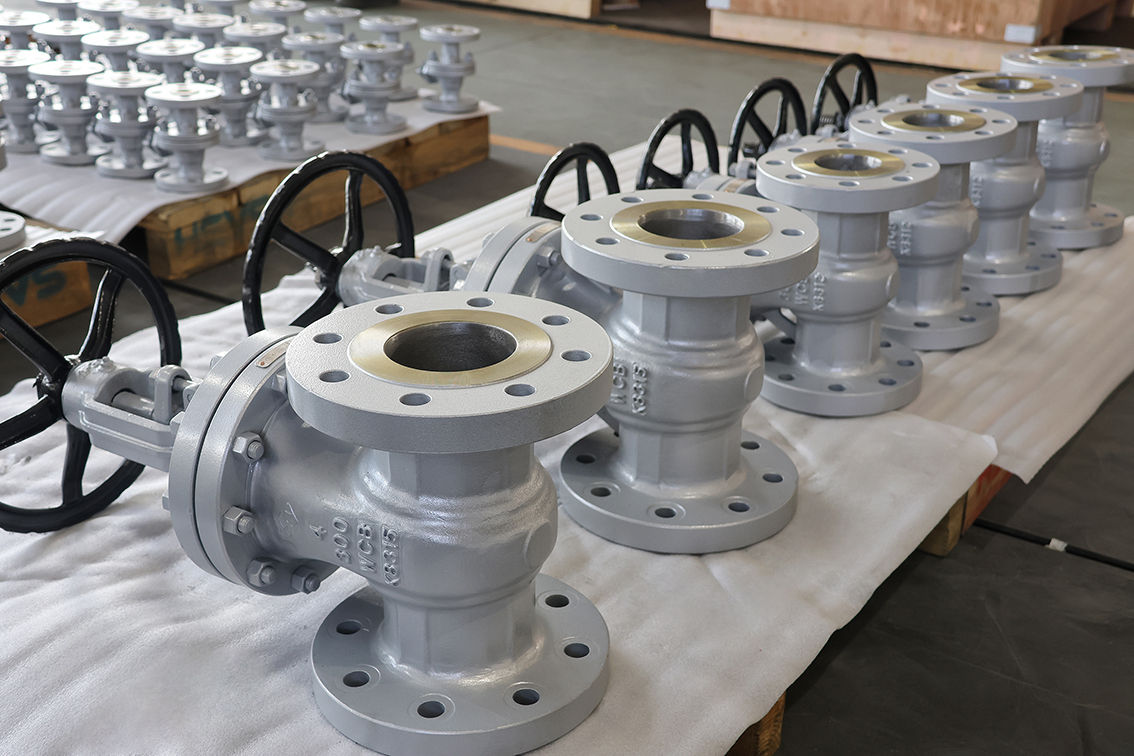
XINTAI Valve’s manufacturing platform incorporates 13 six-axis robots dedicated to polishing and inspection processes. This automation improves production efficiency by 40 percent while ensuring consistent quality and reduced manufacturing variations. Advanced machining and inspection systems deliver micro-level tolerances for demanding flow control applications, a capability that is directly applicable to refinery gate valve performance, where dimensional precision affects sealing integrity and long-term wear resistance. Supporting this manufacturing capability is a dedicated in-house testing facility located in Yongjia, which handles pressure, seal, and material validation.
Integrated Casting and Machining Bases
A defining feature of XINTAI Valve’s operations is internal ownership of casting foundries and machining bases, which enables full-process quality control, optimized costs, and reliable supply stability. This integrated model supports an operational pressure capability of up to Class 2500 and an annual manufacturing capacity of 270,000 valves. Production is distributed across 6 production bases located in Wenzhou, Tianjin, and Lishui, covering a total facility area of 58,800 square meters. The company employs 580 people, including 33 engineers, 41 testers, and 25 quality managers, forming the technical foundation behind consistent valve production at scale.
Gate Valve Engineering for Pipeline Isolation
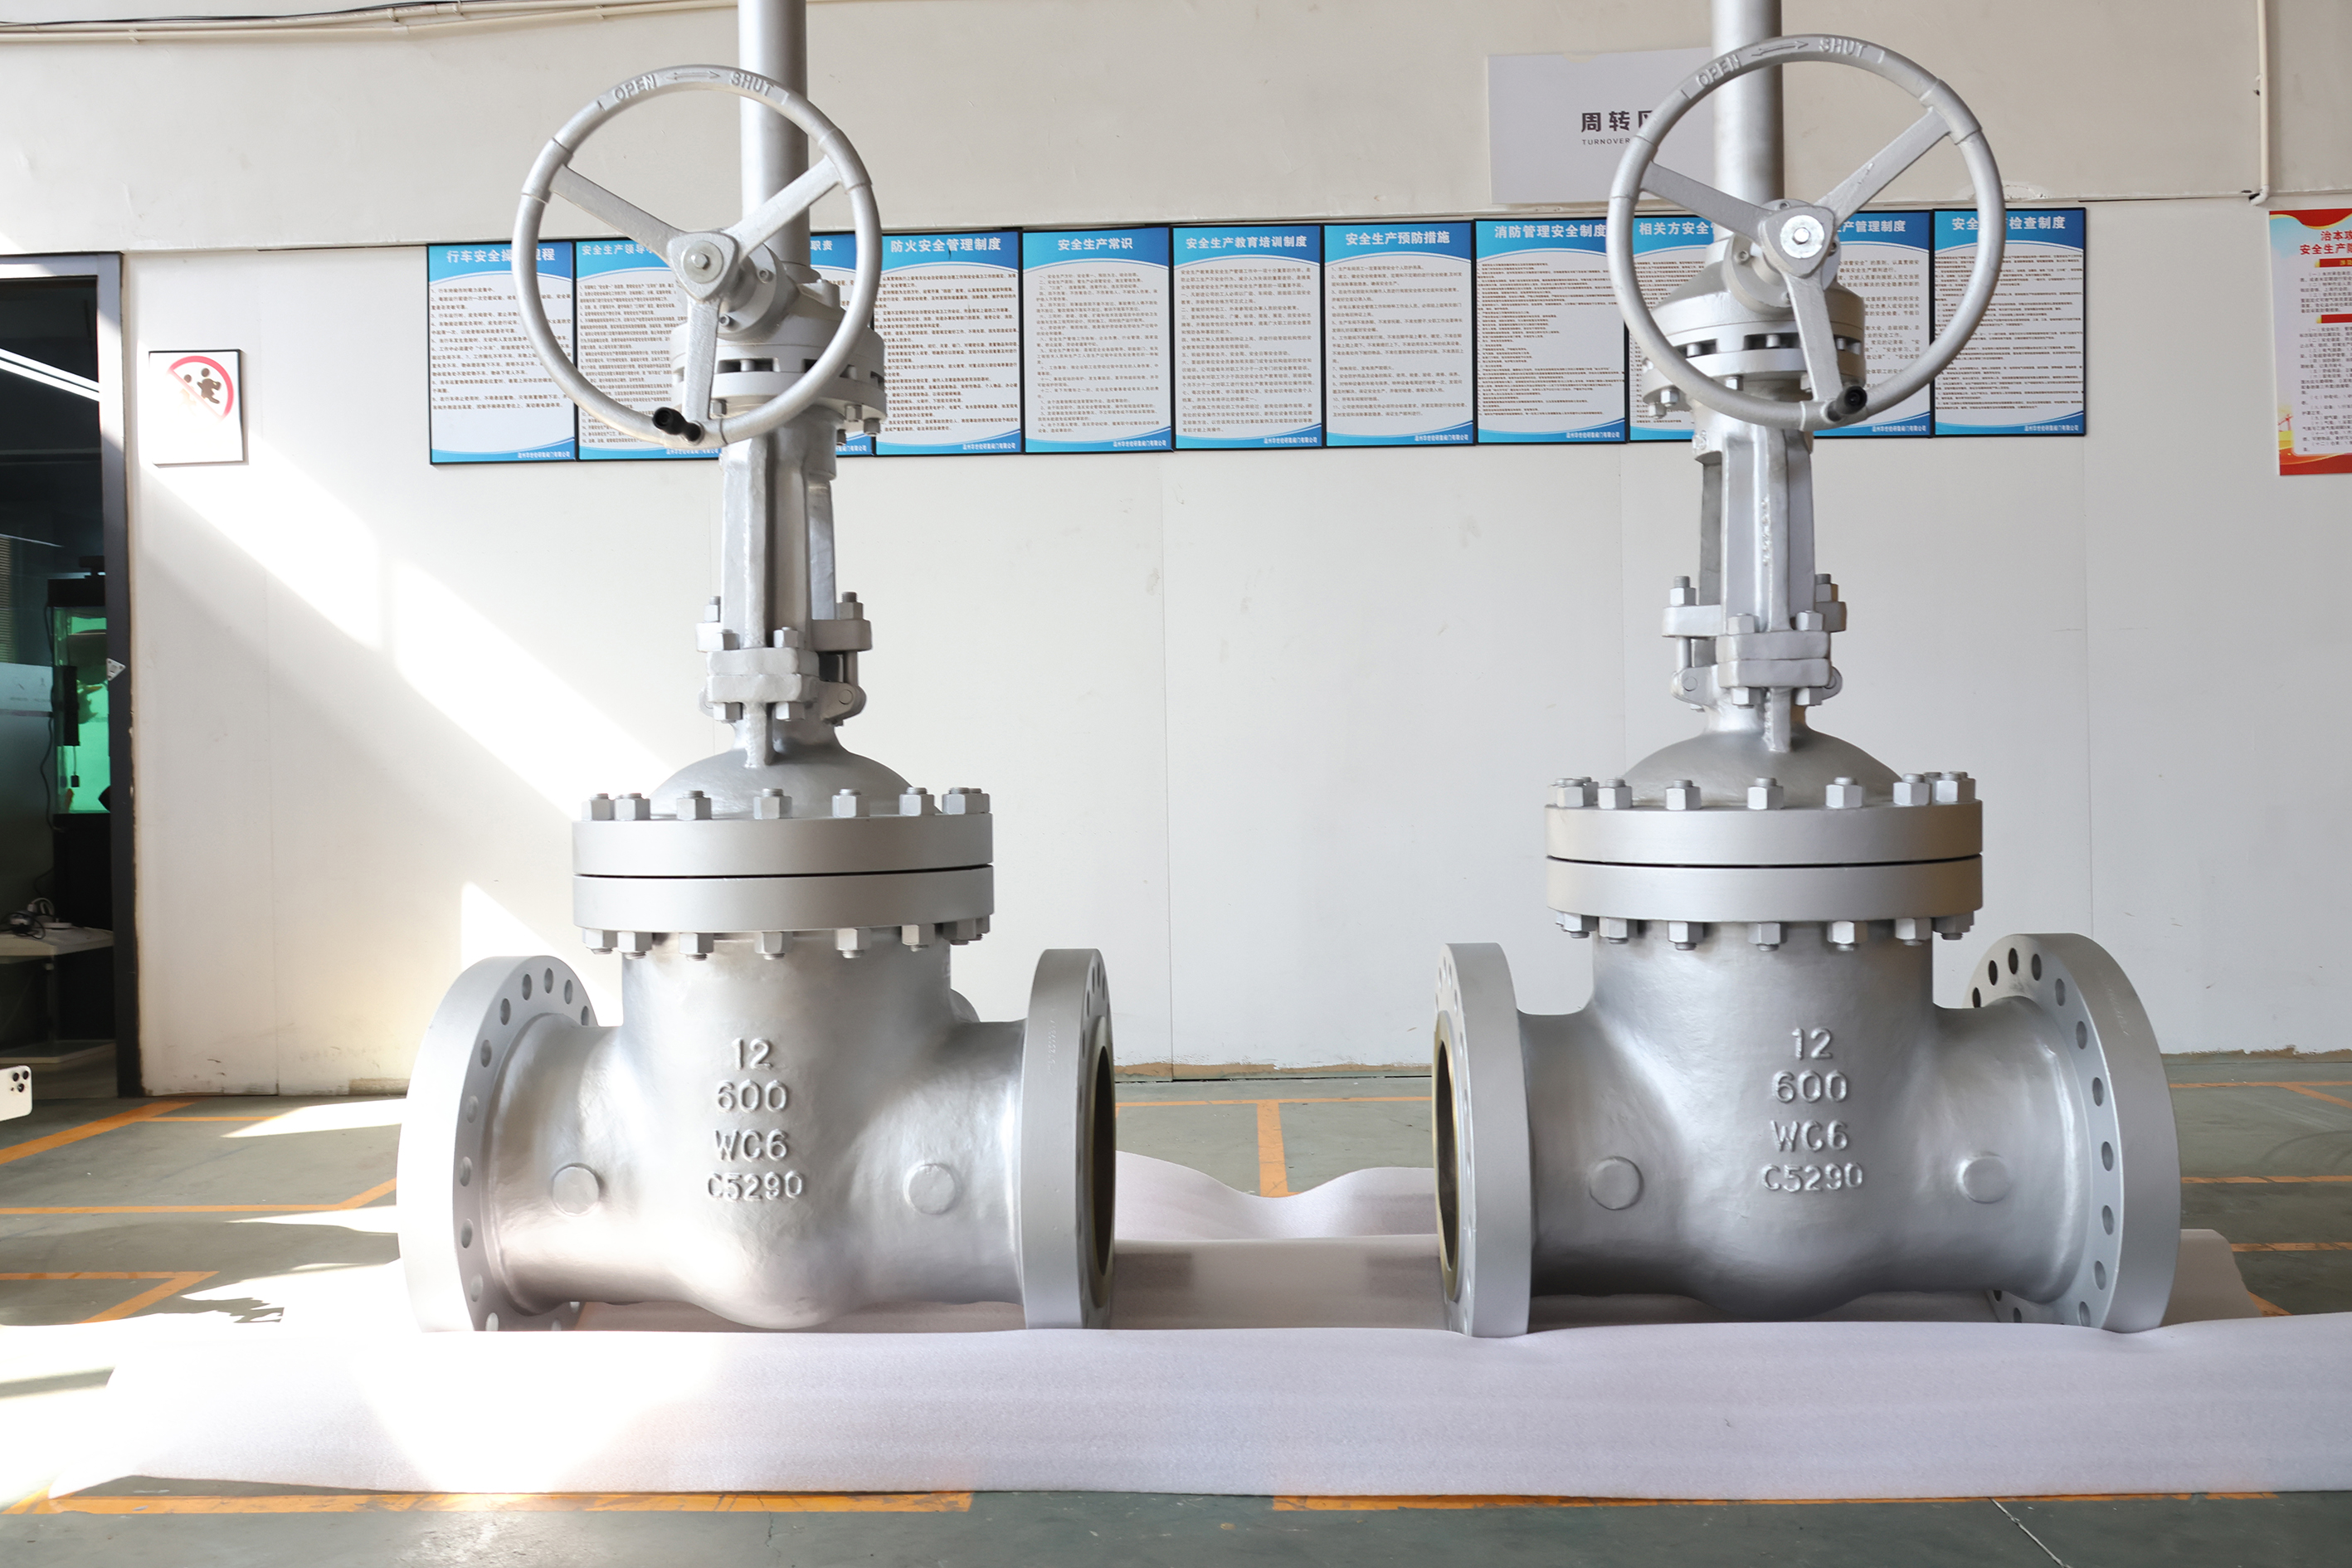
Within its product matrix, XINTAI Valve manufactures Gate Valves in Wedge, Slab, Pressure Seal, Cast Steel, Forged, Rising Stem, Non-Rising Stem, and Knife configurations. These valves are positioned as pipeline isolation valves for full-bore flow control, addressing target scenario pain points such as media leakage to the environment and solid accumulation within pipelines.
The differentiated value of this product line centers on emissions control for hazardous chemical pipelines, where a bellow-sealed design prevents fluid leakage to the environment. Specific engineering features include a wedge gate design that stops fluid flow reliably, a knife gate design with a sharp gate edge that cuts through slurries, pulp, and solid contaminants, and a bellow seal design that provides a secondary metallic barrier to eliminate stem packing leakage. These valves are delivered through a hardware supply model and are adapted for wastewater treatment, chemical processing, and pulp and paper industries, in addition to serving end-user factories such as refineries and power plants among the company’s broader customer base.
Platform compatibility extends to API 6D, API 602, API 600, DIN, JIS, and GOST standards, with support for manual, pneumatic, and electric actuators, allowing gate valves to be specified according to project-specific engineering requirements.
Complementary Valve Portfolio for Complete Flow Control Systems
Beyond gate valves, XINTAI Valve offers a total of 8 product categories, including Ball Valves, Globe Valves, Butterfly Valves, Check Valves, Strainers, Safety Valves, and Cryogenic Valves. This portfolio supports industries covered by the company, including oil and gas, chemical and petrochemical, power plants and power generation, marine and seawater desalination, pulp and paper, district heating, water treatment, and industrial cooling systems. Customer types served include engineering companies, valve trading firms, end-user factories such as refineries and power plants, and distributors.
Proven Global Project Experience
XINTAI Valve’s certified supplier relationships with Petronas and Petrobras illustrate its project experience in competitive international markets. For Petronas, the company supplied valve solutions tailored to regional markets in Southeast Asia. For Petrobras, XINTAI Valve supplied high-specification valves for South American petrochemical projects. On a broader scale, the company’s global export activity shows that 20 percent of products are exported to Europe and the USA, while 80 percent are distributed to other global regions, reflecting the international reach of its hardware supply and custom valve engineering services.
A Dependable Partner for Refinery Flow Control
For engineering firms, distributors, and end-user facilities evaluating a refinery gate valve manufacturer, XINTAI Valve Group Co., Ltd. combines ISO 9001 and CE certification, an integrated casting and machining supply chain, robot-assisted precision manufacturing, and documented project experience with certified international partners. Through its hardware supply and custom valve engineering service models, delivered as physical product supply from its production bases, XINTAI Valve provides refinery operators with a verifiable foundation for sourcing gate valves built to meet demanding pipeline isolation requirements.
www.xintaivalves.com
Xintai Valve Group Co., Ltd.
